INDUSTRIES / SPENT COOLANT
Spent coolant treatment
that cuts what you pay to dispose of.
Spent machining coolant is a stable oil-in-water emulsion that is too strong for a normal effluent plant and is managed as hazardous waste. We test it, break the emulsion, recover the oil, treat the water and help you make your coolant last longer, so there is less to treat in the first place.
In short
What spent coolant is and how it is treated.
Spent coolant is water-mixed metalworking fluid that can no longer be used: an oil-in-water emulsion contaminated with tramp oil, metal fines and bacteria. Its COD is often 20,000 to 80,000 mg/L, far too strong and too toxic for a biological ETP. It is treated by chemical demulsification (acid cracking or coagulants) to split oil from water, oil separation by gravity or DAF, or by ultrafiltration or evaporation, then polishing of the water phase. Under India's Hazardous and Other Wastes Rules, 2016, spent oil and oil-bearing residues need authorisation and must go to an authorised recycler or TSDF.
- 20,000–80,000mg/L
- Typical COD of raw spent coolant
- 3–10%
- Usual working concentration of coolant in water
- 10mg/L
- Oil and grease limit for discharge into inland surface water
- NABL
- Accredited laboratory that characterises your coolant and treated water
What it is
What is spent coolant, and why does it need its own process?
CNC machining, turning, grinding, drilling and honing use a coolant (metalworking fluid) to cool the tool, wash away chips and stop rust. Water-mix coolants are bought as a concentrate and diluted with water, usually to 3 to 10%. There are three main types:
- Soluble oil (emulsifiable oil): mostly mineral oil with emulsifiers; forms a milky emulsion. Easiest of the three to split.
- Semi-synthetic: less oil, more emulsifier and water in the concentrate; a translucent micro-emulsion with fine droplets that is harder to break.
- Synthetic: no mineral oil; a clear solution of synthetic lubricants, amines, corrosion inhibitors and biocides. Little oil to remove, but high dissolved COD that chemicals alone do not take out.
How coolant becomes spent
In use, the coolant picks up tramp oil (hydraulic and slideway oil leaking into the sump), metal fines, hard-water salts and bacteria and fungi. The emulsion weakens, pH falls, the sump smells rancid, machines rust and operators get skin irritation. At that point the sump is dumped, often together with machine and floor wash water.
Why it cannot go straight to the ETP
Coolants are designed to resist breakdown. Emulsifiers keep oil dispersed so it passes through oil traps and settling tanks, and biocides and amines inhibit or kill the bacteria a biological ETP depends on. Diluting it does not help: it spreads the same load, and the hazardous waste question, over more water.
| Parameter | Typical raw range | Usual treated target | Why it matters |
|---|---|---|---|
| pH | 8.0 to 9.5 | 6.5 to 8.5 | Alkaline additives; acid cracking first takes pH down to about 2 to 3 |
| COD | 20,000 to 80,000 mg/L | Below 250 mg/L, or CETP inlet limits | Mostly emulsified oil and additives |
| BOD | 5,000 to 20,000 mg/L | Below 30 mg/L for surface discharge | Low BOD to COD ratio (under 0.3) shows it biodegrades poorly |
| Oil and grease | 5,000 to 20,000 mg/L | Below 10 mg/L | Emulsified, so oil traps alone do not remove it |
| TDS | 5,000 to 15,000 mg/L | As per consent, often 2,100 mg/L | Additives and acid cracking chemicals add salts |
| TSS | 500 to 2,000 mg/L | Below 50 mg/L | Metal fines and swarf; carry metals into sludge |
Rules
Is spent coolant hazardous waste in India?
Spent coolant is a hazardous waste issue as well as an effluent issue. Under the Hazardous and Other Wastes (Management and Transboundary Movement) Rules, 2016, used or spent oil and wastes or residues containing oil are listed in Schedule I, Category 5. The separated oil, oily sludge and any untreated coolant sent off site are handled under these rules; the treated water phase falls under your Water Act consent.
| Requirement | What it means for a generator |
|---|---|
| Classification | Waste cutting oils, used or spent oil and oil-bearing residues fall under Schedule I, Category 5 (5.1 used or spent oil; 5.2 wastes or residues containing oil) |
| Authorisation | Apply to the SPCB in Form 1 for authorisation to generate, store and, if you treat on site, treat hazardous waste |
| Storage | Normally up to 90 days on site, in a marked, bunded and covered area; the board can allow longer in some cases |
| Manifest | A seven-copy, colour-coded manifest (Form 10) travels with every consignment from generator to transporter to receiver, each signing |
| Records and annual return | Keep records of quantities and send the annual return (Form 4) to the SPCB by 30 June each year |
| Disposal or recycling | Only to an SPCB-authorised TSDF, a registered used-oil recycler or re-refiner, or an approved co-processor; transport under the Motor Vehicles Act, 1988 rules |
Treatment
How spent coolant is treated, step by step.
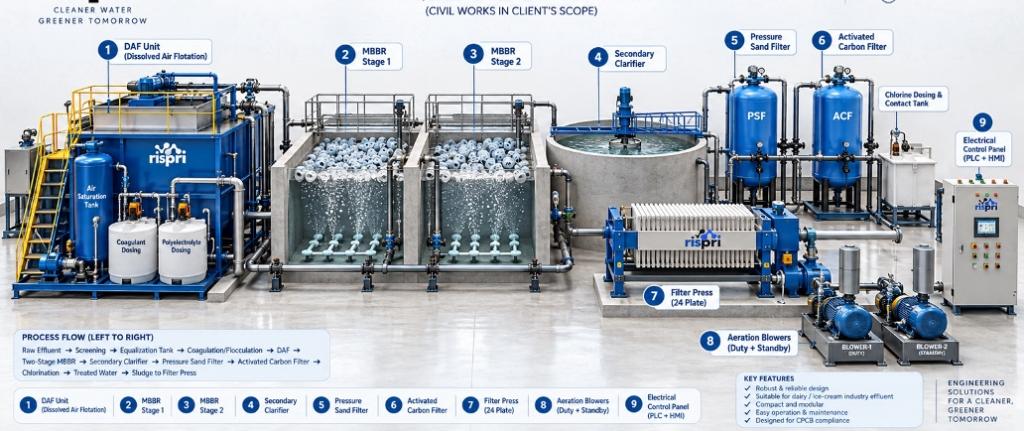
Most plants use a batch system: fill a reaction tank, treat it, separate, and discharge the water phase to polishing. The right chemistry is chosen by jar testing your own coolant.
| Stage | What happens | Notes |
|---|---|---|
| 1. Segregated collection and storage | Spent coolant is collected from sumps into a bunded holding tank, separate from sewage and other effluent. | Skim free tramp oil here; it is the easiest oil to recover |
| 2. Emulsion breaking | Acid cracking (sulphuric acid to pH about 2 to 3, often with heat) or coagulants (alum, PAC, ferric salts) plus organic demulsifiers destabilise the droplets so oil separates. | Typical COD removal is roughly 65 to 97% with alum, 48 to 96% with aluminium chloride and 43 to 93% with iron salts; aluminium usually works better near neutral pH |
| 3. Oil-water separation | Gravity separation, coalescers or dissolved air flotation (DAF) lift the split oil and flocs to the surface. | Coagulation with good separation can remove over 90% of oil and grease even where COD removal is modest |
| 4. Neutralisation and physico-chemical polish | pH is raised, metals are precipitated, and a second coagulation and settling step removes residual oil and solids. | Fe³⁺ and Al³⁺ together have reached just over 80% COD removal with less sludge in published work |
| 5. Sludge dewatering | Oily sludge is dewatered on a filter press to a cake. | Hazardous waste: goes to a TSDF or co-processor under manifest, never with ordinary ETP sludge |
| 6. Final polishing | Activated carbon removes residual COD and colour; a biological stage (often mixed with sewage) handles the remaining biodegradable COD. | A published coagulation, anaerobic hydrolysis and aeration train reached about 99% TOC removal |
| Technology | Best for | Result | Watch-outs |
|---|---|---|---|
| Chemical demulsification + DAF | Soluble oil and semi-synthetic coolants; most plants | Clear water phase; oily sludge | Chemical cost, sludge volume and added TDS |
| Ultrafiltration (UF) | Steady volumes; plants that want little chemistry | Oil-free permeate; small oily concentrate | Membrane fouling; permeate still has dissolved COD from synthetics |
| Vacuum evaporation | Synthetic coolants, mixed oily wastes, sites aiming for no discharge | Distillate for reuse; very small concentrate | Energy use; distillate may carry volatile amines |
| Biological polishing | De-oiled water with biodegradable COD left | Low COD at low running cost | Must be protected from biocides and oil slugs |
Membranes can also recycle coolant itself: published work describes UF membranes of around 100,000 Da and NF membranes of 500 to 2,000 Da used to clean waste coolant for reuse. We also deliver field-proven oily wastewater separation, including graphene membranes and reusable oil-absorbing sponges.
Our NABL-accredited laboratory tests COD, BOD, oil and grease, TSS, TDS, phenols and heavy metals, and runs jar tests to find the demulsifier and dose that work on your coolant before you buy any equipment.
Coolant life extension
The cheapest coolant to treat is the coolant you do not dump.
Every sump you keep running for longer is coolant concentrate you do not buy and spent coolant you do not treat or dispose of. A simple coolant management programme usually pays for itself quickly:
- Control concentration. Check it daily with a refractometer (reading times the coolant's refractometer factor). Too lean causes rust and bacteria; too rich wastes concentrate and irritates skin.
- Use good make-up water. Hard water splits emulsions and forms soap scum. Softened or low-hardness water keeps emulsions stable; see our water softeners.
- Remove tramp oil. Belt or disc skimmers and coalescers take out leaked hydraulic and slideway oil, which feeds bacteria and causes smoke and odour.
- Filter out fines. Paper band filters, magnetic separators, cyclones or centrifuges stop chips and fines from building up.
- Watch pH and bacteria. A falling pH is the first sign of microbial growth. Dip slides show bacteria and fungi; dose biocide only when tests say so.
- Clean sumps properly. When you do change coolant, use a system cleaner so old bacteria do not reinfect the new charge.
Cost
What does spent coolant treatment cost?
Spent coolant volumes are small compared with other effluents, often a few hundred litres to a few kilolitres a day, so the choice is between treating on site and paying to send it away. These ranges help you compare.
| System | Typical capacity | Indicative cost* |
|---|---|---|
| Batch demulsification tank with dosing, separator and small filter press | 0.5 to 3 KLD | ₹8 to 20 lakh |
| Demulsification with DAF and carbon polishing | 2 to 10 KLD | ₹15 to 40 lakh |
| Ultrafiltration unit | 1 to 5 KLD | ₹15 to 45 lakh |
| Vacuum evaporator | 1 to 5 KLD | ₹25 to 80 lakh |
*Indicative 2026 ranges for equipment and installation, excluding civil works, tanks, taxes and the disposal of oil and sludge. Running cost depends mainly on chemicals, sludge disposal and power. We give a firm price after testing your coolant and measuring how much you generate.
Treat on site when
- You generate more than a few hundred litres a day
- Transport and TSDF charges are high in your area
- You already run an ETP or STP for polishing
- You want to reuse water for coolant make-up
Send away when
- Volumes are small and coolant changes are rare
- You have no trained operator for a chemical plant
- A registered recycler near you takes it at fair cost
- Even then, coolant life extension still saves money
We audit your coolant use, set up concentration, skimming and filtration routines, and size the smallest treatment system that pays back.
Troubleshooting
Common spent coolant problems, and how we fix them.
- 01The problem
Coolant was mixed into the ETP and the biology died.
What we doSegregate coolant at source, reseed the ETP, and add a pre-treatment step so the water phase arrives de-oiled.
- 02The problem
The emulsion will not split with the usual chemicals.
What we doJar test acid cracking, mixed coagulants and organic demulsifiers on your coolant; for synthetics, move to UF or evaporation.
- 03The problem
Treated water still fails COD.
What we doAdd carbon or biological polishing for the dissolved COD that chemistry leaves behind.
- 04The problem
Too much sludge, and disposal bills are rising.
What we doOptimise doses, switch to lower-sludge chemistry, improve dewatering, or replace chemical treatment with UF.
- 05The problem
Sumps go rancid and need changing every few weeks.
What we doSet up concentration and pH checks, tramp oil skimming, better make-up water and test-based biocide dosing.
What we offer
What Rispri offers engineering plants.
Oily wastewater treatment
Field-proven separation of oil from water with graphene membranes and reusable absorbents.
Oily wastewater →Coolant and effluent testing
NABL-accredited tests and jar tests for design and compliance.
Testing →Demulsifiers and coagulants
Coagulants, polymers and pH chemicals chosen by jar test.
Chemicals →Effluent treatment plants
ETPs for machining, plating and washing effluent, with oil removal ahead.
ETP solutions →Waste management
Help with storage, records and routes for hazardous and other wastes.
Waste management →Buying guide
What to ask before you buy a coolant treatment system.
Use this list with any supplier, including us.
- Was the chemistry chosen by jar testing my coolant?
- Does it work on all the coolants I use, including synthetics?
- What oil and COD will the treated water contain? In writing.
- How much sludge or concentrate will I still dispose of? In kg per kilolitre.
- What is the cost per kilolitre compared with sending it away?
- Does it fit my hazardous waste authorisation and records?
- Who trains the operator and supplies chemicals?
- Can it also cut how much coolant I dump?
Why Rispri
Testing, chemistry and plant from one team.
Our own NABL lab
We characterise your coolant and certify the treated water, so the designer and the tester work together.
Engineering since 1999
1,498+ plants and turnkey projects for industries, hotels, hospitals and cities.
Chemicals in house
Coagulants and polymers from our own catalogue, tested on your coolant.
Research collaborations
Proven oily wastewater and water technologies, in collaboration with IIT Bombay, IIT Kharagpur and ICT Mumbai.
Questions
Spent coolant treatment FAQs.
What is spent coolant?
Spent coolant is water-mixed metalworking fluid that is no longer fit for use because it has picked up tramp oil, metal fines and bacteria, and its emulsion has weakened. It is a strong oily wastewater, often with COD of 20,000 to 80,000 mg/L.
Is spent coolant hazardous waste in India?
Used or spent oil and wastes or residues containing oil are listed under Schedule I, Category 5 of the Hazardous and Other Wastes Rules, 2016. Spent coolant and the oil and sludge separated from it are therefore managed with SPCB authorisation, records, manifests and disposal to an authorised facility.
Can spent coolant be sent to our ETP?
Not untreated. Its emulsifiers carry oil through the ETP and its biocides can kill the biology. Break the emulsion and remove the oil first; the de-oiled water can then be polished in the ETP.
Can we dilute coolant and discharge it?
No. Dilution does not remove the oil or the toxic additives, and it can put your whole ETP and consent at risk. It also spreads hazardous waste status to more water.
How do you break a coolant emulsion?
Usually by acid cracking (lowering pH to about 2 to 3) or by coagulants such as alum, PAC or ferric salts with organic demulsifiers, followed by gravity separation or DAF. The right chemicals are chosen by jar testing your coolant.
What is the difference between soluble oil, semi-synthetic and synthetic coolant?
Soluble oil is mostly mineral oil and forms a milky emulsion. Semi-synthetic has less oil and finer droplets. Synthetic contains no mineral oil and is a clear solution. Synthetics are often hardest to treat by chemistry alone.
Is ultrafiltration better than chemical treatment?
UF uses little chemistry and leaves a small oily concentrate, but its membranes need cleaning and its permeate can still carry dissolved COD. It suits steady volumes; chemical treatment suits smaller or mixed batches.
How can we make coolant last longer?
Check concentration daily with a refractometer, use soft make-up water, skim tramp oil, filter out fines, watch pH and bacteria, and clean sumps properly when you change coolant.
What tests should be done on spent coolant?
pH, COD, BOD, oil and grease, TSS, TDS, phenols and heavy metals, plus jar tests to choose the demulsifier. Recyclers and TSDFs may ask for further tests on the oil and sludge.
How much does a spent coolant treatment system cost?
As an indication, a small batch demulsification system for 0.5 to 3 KLD costs about ₹8 to 20 lakh, and UF or evaporation systems cost more. We price after testing your coolant and measuring volumes.
What happens to the separated oil?
It is stored as hazardous waste and sent under manifest to a registered used-oil recycler, co-processor or authorised TSDF.
How long can hazardous waste be stored on site?
Normally up to 90 days, in a marked, covered and bunded area with records; the board can allow longer in some cases. Check your authorisation.
Related